Welcome to Taxo Tape
Why Your TIM Datasheet Doesn't Match Real Performance
Introduction
The scenario is familiar to most power electronics engineers who have worked through a thermal design cycle. The thermal model, built around datasheet values from the selected TIM, predicts a junction temperature of 85°C at full load. Hardware testing returns 94°C. The difference isn't explained by measurement error or model simplification — the TIM simply isn't delivering the performance the datasheet implied it would.
This gap between datasheet values and real assembly performance is common enough to be expected rather than surprising. Most of the time, it isn't the result of supplier misrepresentation — it's the result of engineers using datasheet numbers in ways they weren't designed to support: treating typical values as guaranteed minimums, comparing numbers generated by different test methods, or applying laboratory-condition data directly to assembly conditions that differ significantly from the test setup. This article covers where that gap comes from and how to use datasheet data correctly in thermal models and procurement decisions.
Why Datasheet Values Are Not Guaranteed Performance Numbers
The first thing to check on any TIM datasheet is what type of value is being reported, because three different types show up and they mean very different things for design purposes.
Typical values represent the average of measured results from characterized samples — the most commonly reported value type, and the most frequently misused. A typical thermal conductivity of 6.0 W/m·K means the average of the supplier's characterized samples measured 6.0 W/m·K. It doesn't mean every production pad delivers 6.0 W/m·K, or that 6.0 W/m·K is the minimum you should design around.
Minimum values, where reported, define the lower bound the supplier commits to. Designing to a minimum rather than a typical value builds in margin for the production variation that exists below the typical. Many datasheets don't report minimums, which means the typical value is all you have — and using it as a design minimum overstates guaranteed performance.
Specification values appear in some datasheets as the production acceptance threshold — what incoming inspection or QC measures against. These are more reliable design inputs than typical values because they represent a committed threshold rather than an observed average.
There's also a subtler issue worth knowing about: datasheet values are generated from characterized samples, and those samples aren't always representative of the full production population. A supplier who measures conductivity on carefully prepared, freshly produced samples under optimal lab conditions gets a different number than the same measurement run on randomly selected production samples across multiple batches. This isn't deliberate misrepresentation — it reflects that characterization often happens during product development on optimized samples, while production variation is only understood after enough batch history accumulates. When a datasheet reports only typical values with no minimums or specification limits, build your own margin into the design rather than treating the average as guaranteed.
Thermal Conductivity: The Most Commonly Misread Parameter
The W/m·K value on a datasheet is meaningless without knowing how it was measured. ASTM D5470 measures thermal impedance across an actual interface under defined pressure; laser flash diffusivity measures bulk material conductivity with no interface and no compressive load involved. The same physical material, measured by these two methods, can produce values that differ by 20 to 40% — a pad measuring 5.0 W/m·K by ASTM D5470 may measure 7.0 W/m·K by laser flash. Both numbers are technically accurate for what they measure, but only ASTM D5470 reflects something close to what happens at the interface in your actual assembly.
This test-method dependence, along with the pressure sensitivity within ASTM D5470 itself, is covered in more depth in Why Same W/m·K Ratings Perform Differently in TIMs — the short version is: never compare conductivity values across suppliers without first confirming they used the same test method and a comparable test pressure. If the method isn't stated, treat the number as unusable for engineering purposes until you get that confirmation.
Thermal Resistance: Closer to Reality but Still Conditional
Thermal resistance — expressed as °C·cm²/W — integrates conductivity and thickness into a single value that directly represents interface performance, which makes it the more useful number for junction temperature calculations. But the datasheet thermal resistance value still carries conditions that affect how closely it reflects your actual assembly.
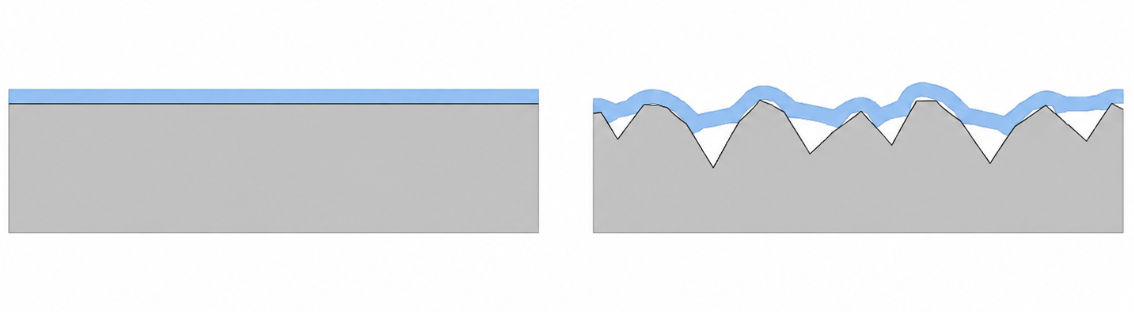
The most significant of these is surface finish. ASTM D5470 test fixtures use lapped metal surfaces with Ra values typically below 0.1 µm — smoother than almost any production heatsink surface. Contact resistance at the TIM-to-metal interface decreases as surface roughness decreases, which means the datasheet value reflects better surface contact than your assembly will actually achieve. Production heatsink surfaces range from Ra 0.4 µm for finish-machined aluminum up to Ra 3.0 µm or higher for as-cast or as-extruded surfaces — a meaningfully rougher condition than the test fixture.
Combine that surface finish gap with production clamping pressure variation — typically ±20 to 30% from nominal torque without torque-controlled tooling — and the combined effect commonly adds 10 to 25% to the datasheet thermal resistance value in real assemblies. For a design with tight thermal budget headroom, that gap is often the difference between a design that works in hardware and one that doesn't. Contact resistance specifically — the additional resistance from surface roughness and TIM hardness at the interface — can account for 20 to 40% of total interface resistance on rough heatsink surfaces, and it's rarely broken out separately on standard datasheets. Softer, more conformable pads reduce this contribution by deforming into surface irregularities more readily, which is one reason a softer 4.0 W/m·K pad sometimes outperforms a stiffer 6.0 W/m·K pad in actual hardware.
Thickness and Dimensional Tolerances
A thermal pad specified at 1.0mm nominal thickness with ±10% tolerance covers a range from 0.9mm to 1.1mm. That 0.2mm total range sounds modest, but for a material with 5.0 W/m·K conductivity, the difference in bulk thermal resistance between the two ends of that range is roughly 0.04 °C·cm²/W — small in absolute terms, but meaningful when total TIM resistance in the design is only around 0.20 °C·cm²/W.
More importantly, thickness tolerance describes a production population, not a unit-level guarantee. A batch where most pads cluster near the upper end of the tolerance band produces systematically higher thermal resistance than the nominal datasheet value predicts, without any individual pad being out of spec. This matters more once you account for compression: nominal pad thickness and bond line thickness (BLT) are different quantities, since BLT is the compressed thickness under actual clamping pressure. A pad starting at 1.1mm and compressing 15% produces a BLT of 0.935mm; the same batch's pad starting at 0.9mm and compressing the same 15% produces a BLT of 0.765mm — a 0.17mm difference between two units that are both within specification.
This is why thermal models built around a single nominal BLT don't accurately represent production performance distribution. A more reliable approach models worst-case BLT — the upper end of thickness tolerance combined with the lower end of the compression range — and verifies junction temperature stays acceptable even at that condition. The compression stress-versus-thickness curve, where available, tells you more about real assembly BLT than the nominal thickness spec alone: a pad with a flat compression curve accommodates thickness variation more gracefully than one with a steep curve that resists compression strongly.
Parameters That Datasheets Often Omit
A handful of parameters that matter most for long-term reliability are absent from most commercial TIM datasheets — not usually by accident, but because they're inconvenient to measure and don't always favor commercial positioning.
Compression set — the permanent thickness reduction that remains after sustained load is removed — is the parameter most relevant to long-term interface stability in sealed assemblies, and it's missing from the majority of datasheets. Standard test methods require 22 to 70 hours of sustained load at elevated temperature, and a pad showing 20% compression set after 70 hours at 125°C ends up 0.2mm thinner after extended service if it started at 1.0mm — directly increasing BLT and thermal resistance over the product's life.
Aging behavior at operating temperature is similarly absent. Silicone-based pads can experience cross-link density changes that alter hardness and compressibility over time; dispensed gap fillers can undergo partial volatilization that changes mechanical and thermal properties. Standard datasheets report fresh, unaged material — for a sealed assembly running continuous duty for years, the material's properties at year five matter more than its properties at day one.
Batch-to-batch variation in thermal conductivity of ±10 to 15% isn't unusual in commercial TIM production, reflecting filler loading variation and process drift over time. For a nominal 6.0 W/m·K material, that range means production batches may actually deliver anywhere from 5.1 to 6.9 W/m·K — a spread that matters if your thermal budget is tight.
Surface finish sensitivity — how much thermal resistance increases as heatsink roughness moves from the smooth test fixture condition to your actual production surface — also goes unreported. This sensitivity varies significantly by TIM type: soft, conformable pads accommodate roughness through elastic deformation with relatively low sensitivity, while harder pads bridge surface peaks without filling valleys, producing stronger sensitivity to surface finish.
For any of these four parameters, if the supplier can't provide the data, the safest approach is to treat that aspect of long-term performance as uncharacterized rather than assuming it falls within an acceptable range.
How to Use Datasheet Values Correctly
The practical starting point is treating datasheet thermal conductivity and thermal resistance values as optimistic estimates rather than conservative design inputs. For thermal models used to verify junction temperature headroom, apply a correction factor of 1.15 to 1.25 to the datasheet thermal resistance at nominal BLT — this range accounts for the typical gap between lab test conditions and production assembly conditions covered in sections 4 and 5.
If the model shows adequate junction temperature margin after applying this correction, the design has reasonable robustness to real-world assembly variation. If it only passes without the correction, the design is relying on best-case datasheet performance and will likely show thermal margin problems once it reaches hardware.
Not every parameter requires independent verification — dimensions, hardness, and electrical insulation can generally be confirmed through incoming inspection. Thermal resistance, however, needs to be verified in your actual assembly under your actual conditions; no amount of datasheet analysis substitutes for that measurement. BLT under real assembly conditions should also be measured on a sample basis during qualification, not calculated from nominal pad thickness alone.
Building a Verification Protocol
A standard verification protocol for a new TIM specification should run three steps in sequence before production commitment.
First, datasheet review with the correction factor applied to the thermal model — confirming the design passes with realistic inputs, not best-case ones. Second, first article inspection of samples against specified dimensional and mechanical tolerances. Third, thermal resistance measurement in hardware under production-representative conditions, on a sample of five or more units rather than a single sample.
This protocol adds one to two weeks to a qualification timeline, but it catches the most common sources of datasheet-to-reality divergence before they show up in production. For any assembly where a field thermal issue would mean rework or returns, that time investment is straightforward to justify.
Working with Your TIM Supplier
Getting a supplier to provide the data covered in section 6 — compression set, aging behavior, batch variation, surface finish sensitivity — usually comes down to asking directly rather than assuming it doesn't exist. Suppliers with mature, well-characterized product lines typically have this data available even when it isn't printed on the standard datasheet; it just isn't volunteered unless requested.
Before finalizing a TIM specification for a critical or long-life application, request: the specific test method and pressure behind the conductivity and thermal resistance values, batch test data from multiple recent production lots, and compression set or aging data if your application involves sustained elevated temperature or a multi-year service target. For a fuller framework on qualifying a TIM supplier before committing to production volume — including what documentation to request and how to structure sample validation — see How to Validate a TIM Supplier.
FAQ
Q: What should I use as a design input if the supplier only provides typical values, no minimums?
Apply your own margin rather than designing to the typical value directly. A correction factor of 1.15 to 1.25 on thermal resistance, as covered in section 7, is a reasonable starting point absent supplier-specific minimum data — and if the application is critical enough, request the supplier's internal production specification limits rather than relying on the typical value from the public datasheet.
Q: The supplier doesn't have compression set data — how should I handle that?
Treat long-term thermal stability as uncharacterized rather than assuming acceptable performance. For a short service-life or serviceable application, this may be an acceptable risk. For a sealed, multi-year application, either request the supplier commission the testing, source independent testing on samples, or consider a supplier who already has this data for a comparable product.
Q: How much of the datasheet-to-reality gap is really about surface finish?
It's frequently the single largest contributor, particularly on as-cast or as-extruded heatsink surfaces rather than finish-machined ones. Combined with realistic clamping pressure variation, surface finish effects commonly account for most of the 10–25% gap described in section 4 — which is why hardware verification on your actual heatsink surface matters more than refining the thermal model further.
Conclusion
Datasheet values for thermal interface materials are useful starting points — they define a material's performance tier and support initial supplier comparison — but they aren't guarantees of what happens at the interface in your specific assembly. Treating them as guarantees is one of the more reliable ways to end up with a thermal design that passes simulation and then runs hot in hardware.
The gap between datasheet and reality comes from identifiable, predictable sources: test method and pressure dependence in conductivity values, surface finish and contact resistance effects not captured in reported thermal resistance, thickness tolerance effects on BLT distribution across a production population, and long-term parameters — compression set, aging, batch variation — that standard datasheets routinely omit. Understanding where the gap comes from is what makes it manageable: apply realistic correction factors in thermal models, verify performance in hardware before committing to production, and request the data suppliers don't volunteer by default.
For a closer look at why nominally identical conductivity ratings can perform differently across suppliers, see Why Same W/m·K Ratings Perform Differently in TIMs. For the qualification process that turns hardware verification into a production release decision, see How to Validate a TIM Supplier.